
Komatsu | 30,000 Hours of Clean Hauling
Proven reliability in high-horsepower mining applications
Proven results
The Challenge
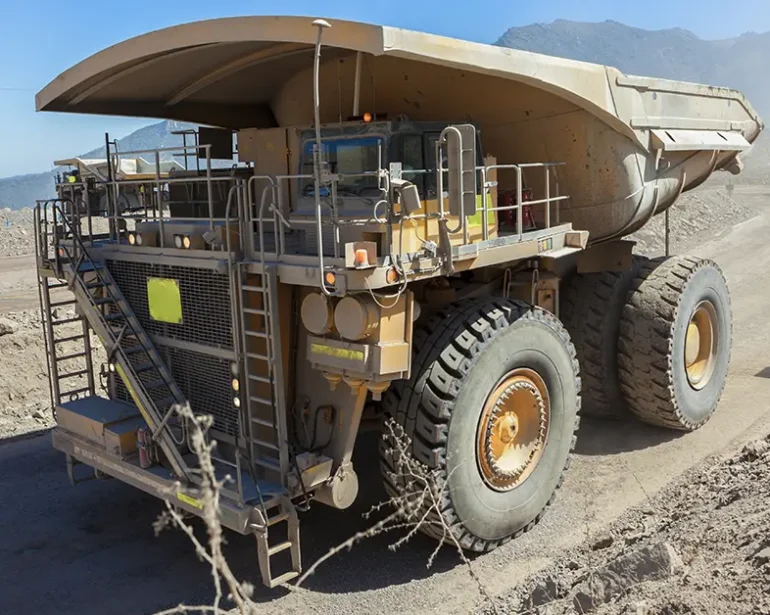
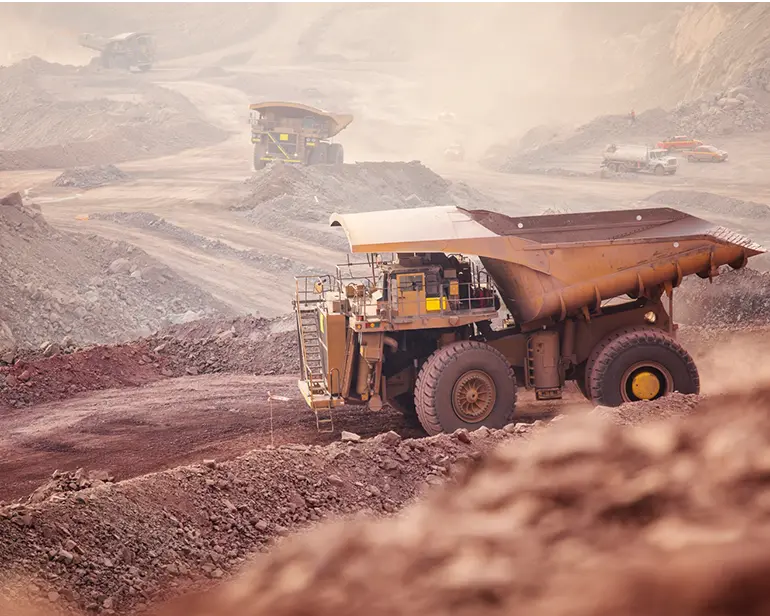
At Chile’s Los Pelambres mine, Komatsu’s 930E 300-tonne haul trucks, powered by 2,700 hp Cummins QSK60 engines, were plagued by fuel contamination.
Blocked filters led to severe downtime, costly repairs and reduced machine productivity in one of the world’s most demanding mining environments.
The Solution
FuelActive engineered a bespoke High Horse Power (HHP) fuel pick-up system tailored for Komatsu’s 930E haul trucks. Installed directly into the fuel tanks, the floating unit continuously delivered clean diesel to the QSK60 engine, preventing contaminants from entering the system.
The results were immediate: fuel filters consistently reached and often exceeded their target maintenance intervals, extending from 500 hours to as much as 1,000 hours between changes.

“FuelActive’s design transformed reliability in our high-horsepower fleet. Cleaner fuel means fewer breakdowns, lower costs and maximum uptime for our customers.”
The Benefit
With FuelActive fitted, Komatsu Cummins eliminated fuel contamination issues entirely. The 930E fleet achieved over 30,000 hours of trouble-free operation, reducing maintenance costs, extending component life and maximising uptime.
The system’s reliability has enhanced fuel efficiency and operational continuity in high-dust, high-demand conditions, reinforcing the value of clean-fuel delivery in large-scale mining applications.
The Outcome

Reliability
30,000+ hours of continuous operation

Maintenance saving
Fewer filter changes and component failures

Sustainability
Cleaner combustion reduces emissions and fuel waste

Efficiency
Extended operating time and machine availability
Built for the toughest conditions.
See how FuelActive protects high-performance mining engines from contamination and downtime.
